
Direct Answer
Design for Manufacturing (DFM), also called design for manufacturability, is the practice of designing a part or product around the realities of how it will actually be produced. The goal is to satisfy required function and performance while eliminating geometry, tolerances, tooling demands, setups, materials, inspection requirements, or secondary operations that create unnecessary manufacturing difficulty.
DFM is therefore not a universal list of rules such as “add a radius” or “loosen every tolerance.” A good DFM decision depends on the intended manufacturing process, material, production quantity, available equipment, supplier capability, inspection method, and the features that actually control product function. NIST describes manufacturability analysis as identifying potential manufacturing problems during the design phase so designers can correct them before production, while ASME emphasizes integrating manufacturing decisions without sacrificing functionality and performance.
How to Perform a Design for Manufacturing Review
A useful DFM review starts with the part’s required function and then tests whether the proposed manufacturing route can produce, inspect, and repeat that function without avoidable manufacturing burden.
Function, critical interfaces, expected production quantity, material needs, and the likely manufacturing process.
Process-specific checks for geometry, tooling and fixture access, tolerances, finishing, secondary operations, and inspection.
The revised design still meets its functional requirements and can be produced repeatedly with the intended supplier, equipment, and quality plan.
| Review Area | Question to Answer | Warning Sign | DFM Action |
|---|---|---|---|
| Function | Which surfaces, dimensions, features, and interfaces actually control performance? | A proposed manufacturing change alters a load path, locating feature, sealing surface, fit, motion, or other required function. | Protect functional requirements before optimizing manufacturing. |
| Production quantity | Is the part a prototype, low-volume component, or production item? | The process or tooling investment was chosen without considering how many parts must be made. | Compare tooling, setup, cycle, and per-part implications at the expected volume. |
| Manufacturing process | What process will create the primary geometry? | Detailed geometry is finalized before machining, molding, forming, casting, fabrication, or additive constraints are considered. | Select or shortlist the production route before locking process-sensitive geometry. |
| Material and stock | Is the material appropriate for both function and the intended process? | The material satisfies strength or corrosion requirements but creates avoidable manufacturing, sourcing, heat-treatment, or finishing problems. | Review material form, availability, machinability/formability, joining, treatment, and process compatibility. |
| Geometry | Can required features be produced directly and repeatably? | Hidden features, deep pockets, undercuts, difficult transitions, or unnecessary complexity require special operations. | Simplify nonfunctional geometry while preserving required interfaces. |
| Tool and fixture access | Can tools, fixtures, clamps, probes, fasteners, and inspection equipment physically reach the required features? | A feature looks accessible in CAD but requires an awkward setup, long tool, special fixture, or impossible assembly approach. | Improve access, orientation, datum strategy, or feature placement. |
| Tolerances | Which dimensional and geometric variations actually affect function? | Blanket tight tolerances or unnecessarily restrictive controls appear across noncritical features. | Allocate tolerances from functional requirements and process capability. |
| Inspection | Can the specified requirements be measured economically and repeatably? | A critical feature lacks practical datum access, gauge access, or a clear inspection method. | Resolve the datum scheme, measurement approach, and acceptance requirement before release. |
| Secondary operations | Which deburring, finishing, coating, heat treatment, joining, cleaning, or inspection operations remain after the primary process? | Many secondary operations exist only because of avoidable design choices. | Consolidate or eliminate operations where function permits. |
| Supplier capability | Can the actual manufacturing source repeatedly produce the design? | The design relies on generic process assumptions rather than real equipment, tooling, inspection, or supplier capability. | Close the review with manufacturing feedback and capability confirmation. |
Swipe horizontally to view all table columns.
Ask progressively: Can it be made? Can it be made with the intended process? Can the available manufacturer and equipment make it? Can the result be inspected and repeated? Can it be produced economically at the required volume? A design that passes only the first question is technically manufacturable, but it may still be poor DFM.
DFM vs. DFA vs. DFMA
DFM primarily addresses how parts and products are manufactured. Design for Assembly (DFA) concentrates on how components are handled, oriented, located, joined, fastened, and assembled. DFMA combines manufacturing and assembly considerations. A molded housing may have excellent DFM for molding yet still have poor DFA if internal fasteners cannot be reached during assembly.
For assembly-focused decisions such as part count, fastener access, alignment, and assembly sequence, continue with the Turn2Engineering Design for Assembly guide. For the broader development sequence that places DFM before controlled release, see the mechanical engineering design process.
Research basis: NIST — Automated Manufacturability Analysis: A Survey describes manufacturability analysis as a way to identify potential manufacturing problems during design and provide feedback for correcting them before production.
How the Manufacturing Process Changes the Design
A geometry is not inherently “good for manufacturing.” It is good or poor relative to a specific process, material, production quantity, tooling approach, and manufacturing capability.
A machined component is created by removing material with accessible cutting tools. A formed sheet-metal component begins with nearly constant-thickness stock and gains stiffness through bends and formed geometry. A molded or cast component must be created and released from tooling. An additive component is built layer by layer but can still be constrained by orientation, supports, surface finish, thermal distortion, post-processing, and inspection. Changing the process can therefore change the best geometry even when the required function stays the same.
The figure below illustrates the concept. Focus on the structural differences between the variants rather than treating any numerical annotation in the illustration as a universal design rule. Draft, radii, wall proportions, bend details, machining allowances, and similar process limits must be confirmed for the actual material, process, tooling, and manufacturer.

| Process | Geometry Questions | Tooling / Setup Questions | Typical DFM Focus | Verify Before Release |
|---|---|---|---|---|
| CNC machining | Can cutters reach pockets, holes, shoulders, corners, and finishing surfaces? | How many orientations, fixtures, tool changes, and long-reach operations are required? | Tool access, setups, internal geometry, stock removal, tolerance burden. | Machine capability, tool strategy, workholding, datum transfer, inspection. |
| Injection molding | Can the part fill, cool, and release from the mold without avoidable tooling complexity? | Where is the parting strategy, and do undercuts require additional tooling actions? | Wall transitions, draft, ribs, bosses, coring, ejection, tooling access. | Resin, mold design, shrinkage assumptions, cosmetic surfaces, tolerance capability. |
| Sheet metal | Can the geometry be created from sheet stock through feasible cutting and forming operations? | Can the part be held and bent in the required sequence without tool interference? | Bend sequence, bend/tool access, reliefs, feature placement, flat pattern. | Material condition, thickness, tooling, bend process, downstream distortion. |
| Casting | Can the geometry be formed, filled, removed, cleaned, and finished using the selected casting route? | What cores, mold features, gates, risers, draft, machining allowances, or secondary operations are needed? | Section transitions, tooling complexity, cores, distortion, critical machined interfaces. | Specific casting process, alloy, foundry capability, machining and inspection plan. |
| Additive manufacturing | How do orientation, overhangs, trapped material, internal channels, and post-processing affect the part? | What support, removal, finishing, machining, heat treatment, or build setup is required? | Build orientation, supports, accessibility, distortion, surface and datum strategy. | Machine/process, material, build parameters, post-processing and qualification requirements. |
| Welded fabrication | Can components be cut, located, welded, and subsequently machined where needed? | Can the joint be accessed, fixtured, sequenced, and inspected? | Joint access, distortion, fixture strategy, weld sequence, post-weld machining. | Welding process, material, distortion allowance, inspection and applicable requirements. |
Swipe horizontally to view all table columns.
A process decision also changes the economics. Tool-intensive processes can become attractive when tooling cost is distributed over sufficient production quantity, while machining or additive manufacturing may avoid major dedicated tooling for prototypes or lower-volume work. That does not create a universal volume breakpoint; quotes, tooling life, cycle time, material utilization, quality requirements, and supplier capability determine the actual crossover.
If material and process are still being selected together, use the Material Selection guide to evaluate mechanical properties, environment, manufacturability, availability, and lifecycle requirements as one decision rather than choosing a material from strength alone.
Professional guidance: ASME — How to Apply Design for Manufacturing Principles to Your Project identifies material cost and availability, retooling, manufacturing collaboration, tolerances, compliance, and testing among the considerations that complicate DFM decisions.
Geometry, Tooling, and Access: Where DFM Problems Begin
DFM geometry should let the selected process create the required features with practical tool, fixture, assembly, and inspection access while avoiding complexity that does not contribute to function.
CAD makes complex geometry easy to draw, but the manufacturing route still determines which surfaces can be generated directly, how the workpiece must be held, what tool approaches are available, and how often the part must be repositioned. A small geometric change can therefore eliminate an entire setup or special tool even though the finished component performs the same function.
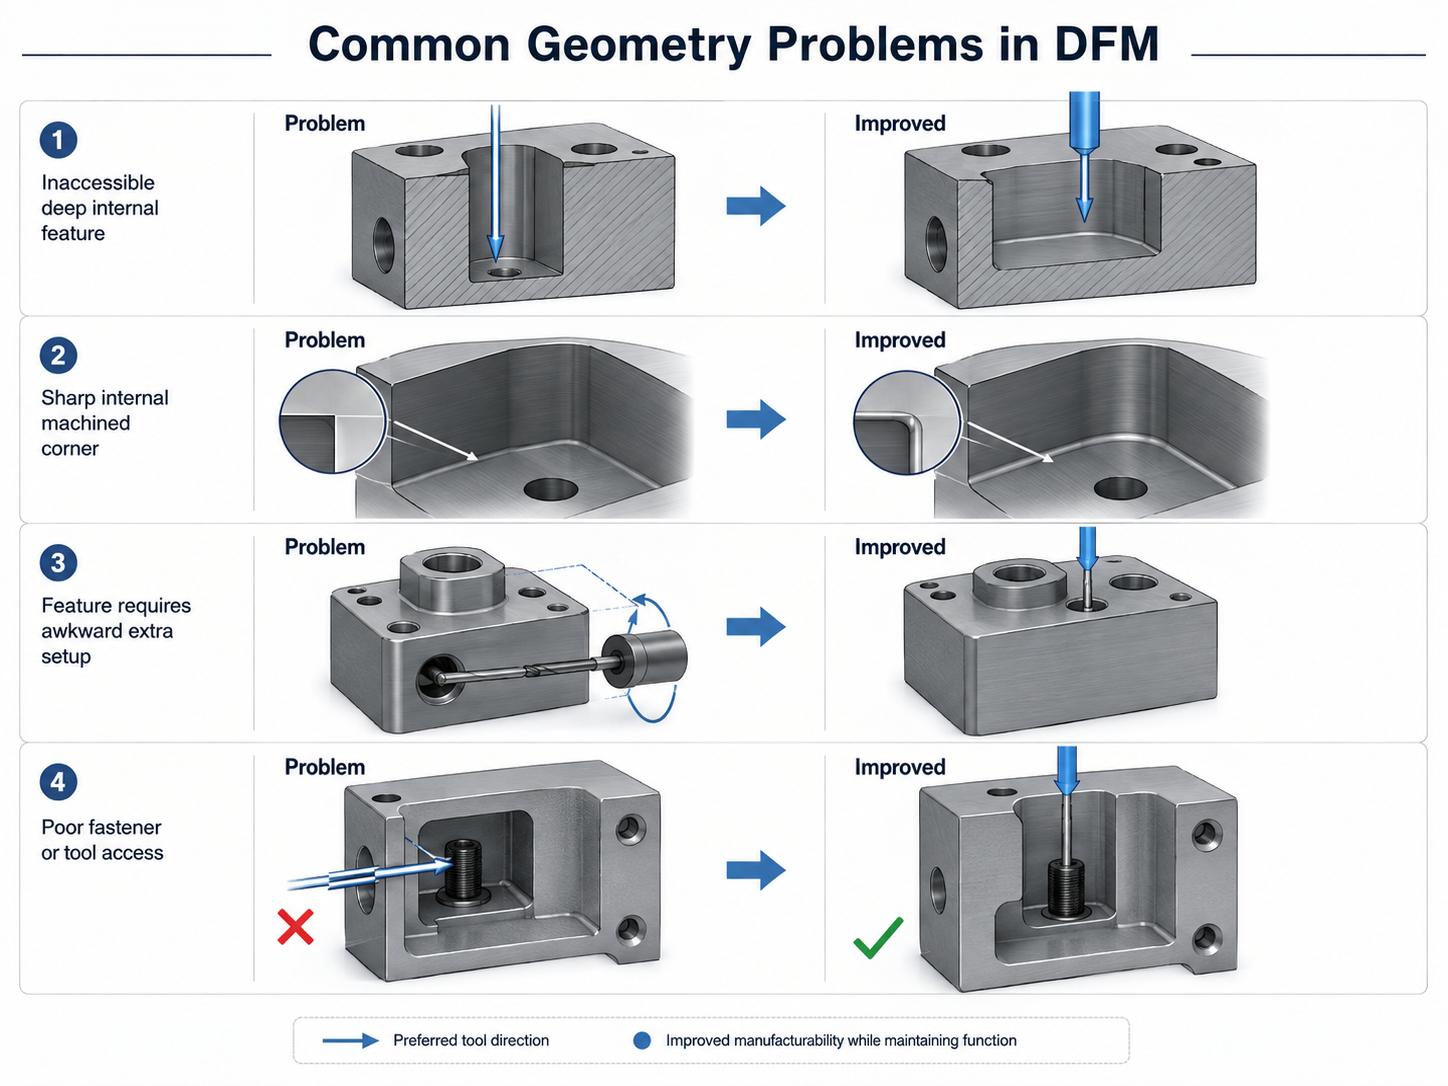
Design the feature around the real tool approach
For machining, ask how the cutter reaches the feature and how the part is held while that happens. A pocket that is visually open from an isometric CAD view may still require a long tool, awkward side operation, or additional fixture orientation. Likewise, fasteners and service features should be checked using the envelope of the real installation tool, not only the nominal fastener geometry.
Do not specify geometry a process cannot directly create
A rotating milling cutter naturally leaves an internal radius. A sharp internal corner in a machined pocket therefore either requires a different manufacturing approach, a secondary operation, or a design change. The DFM question is not simply “Can the drawing show a sharp corner?” but “Does function require that exact corner condition, and what operation will create it?”
Treat every setup change as a design question
Additional orientations can require new workholding, datum transfer, operator handling, probing, inspection, and machine time. Some setups are unavoidable because of function. Others exist because one noncritical feature faces a different direction from the rest of the manufacturable geometry. During DFM, identify which features drive each setup and ask whether their orientation or form can change.
Check fixture and inspection access, not only cutting access
A part must be held before it can be machined and referenced before it can be measured. Preserve stable locating and clamping surfaces, avoid creating a geometry that becomes difficult to restrain after an early operation, and consider how critical features will be inspected. Manufacturing and inspection should reference a coherent design definition rather than forcing the shop to invent an uncontrolled datum strategy.
For every difficult feature, ask: What requirement forces this geometry? If the answer is unclear, the feature is a candidate for simplification. If the requirement is real, optimize the manufacturing method around the requirement instead of deleting the feature merely to reduce cost.
Tolerances, Surface Finish, and Inspection in DFM
Specify dimensional, geometric, and surface requirements from function and verification needs—not from the maximum precision a drawing system allows.
Every manufacturing process produces variation. DFM does not remove that variation; it creates a design that works with controlled variation. The first step is to identify the dimensions and geometric relationships that govern fit, alignment, sealing, motion, load transfer, interchangeability, appearance, or another measurable requirement. Those features deserve deliberate tolerancing. Noncritical geometry should not inherit unnecessarily restrictive limits merely because nearby critical geometry is precise.
Tie tolerance to a functional failure mode
For a locating hole pattern, the controlling concern may be assembly alignment. For a bearing seat, it may be fit, position, or runout. For a sealing face, it may be flatness, finish, or relative location. If the designer cannot explain what goes wrong when a tolerance is exceeded, the control may not yet be connected to design intent.
When geometric relationships matter, the Turn2Engineering GD&T guide explains how datum reference frames and geometric controls communicate permissible variation. When several dimensions combine to determine a gap, clearance, preload, alignment, or fit, use Tolerance Stack Up Analysis rather than tightening each contributing dimension independently.
Specify surface finish where the surface function requires it
Surface requirements can influence machining operations, tooling, process sequence, finishing, measurement, and cost. Distinguish a functional bearing, sealing, sliding, fatigue-sensitive, optical, or cosmetic surface from an ordinary noncritical face. Avoid applying the same finish requirement to every surface unless the product genuinely requires it.
Design the requirement so it can be inspected
A technically valid requirement can still be poor production engineering if it cannot be measured repeatably with the planned inspection method. During DFM, ask how the part will be oriented for inspection, which datums establish the measurement, whether probes or gauges can reach the controlled features, and whether the inspection method matches the tolerance being specified.
Pass condition: The requirement is traceable to a specific functional need.
Evidence: Calculation, interface analysis, test requirement, tolerance analysis, or documented design criterion.
If it fails: Reconsider the tolerance or the design requirement before release.
Pass condition: The requirement can be measured repeatably using the intended production inspection approach.
Evidence: Defined datum setup, gauge/CMM strategy, fixture concept, or supplier inspection plan.
If it fails: Change the datum scheme, feature definition, access, tolerance, or verification method.
The Turn2Engineering GD&T resource explains the design-intent relationship between geometric controls, datums, allowable variation, and practical inspection; the Tolerance Stack Up Analysis guide addresses how multiple manufacturing variations combine at assembly level.
DFM Worked Example: Redesigning a Machined Bracket
Consider a machined mounting bracket with a required base interface, a large locating bore, mounting holes, and a smaller raised locating feature. The detailed dimensions, material, loads, production quantity, and tolerances are intentionally not prescribed here; those values must come from the actual project. The purpose of the example is to show the decision sequence.

- 1. Freeze the functional requirements before simplifying geometry: Identify the mounting surfaces, hole pattern, locating bore, raised locating feature, load path, alignment needs, surrounding envelope, and any required service access. Those requirements define which geometry may not be changed casually.
- 2. Identify what drives manufacturing effort: On the original concept, deep and fragmented pockets, internal transitions, isolated features, and differently oriented operations can increase tool travel, programming, fixturing, workholding, or setup complexity. Each difficult feature should have a functional justification.
- 3. Simplify nonfunctional material removal: Replace a collection of narrow pockets and isolated recesses with broader, tool-accessible regions where stiffness, mass, clearance, and load-path requirements permit. Use geometry that can be reached with practical cutting tools instead of requiring special approaches solely to reproduce CAD detail.
- 4. Preserve the interfaces that control function: Maintain the mounting pattern, locating bore, critical base surfaces, alignment features, and other interfaces that connect the bracket to the machine. DFM is not successful if easier machining destroys the bracket’s actual job.
- 5. Revisit the tolerance scheme: Separate critical locating, alignment, and mating requirements from noncritical pocket or exterior dimensions. Use the functional tolerance chain to determine where precision is needed instead of applying tight tolerances broadly.
- 6. Define inspection while the geometry is still flexible: Confirm that the selected datums and critical features can be reached and measured using the intended inspection method. A datum or controlled surface that is difficult to establish can force an avoidable inspection fixture or redesign.
- 7. Return the redesign to engineering analysis: Simplifying pockets or ribs changes mass, stiffness, stress distribution, natural frequency, thermal behavior, and possibly fatigue performance. Recheck the engineering requirements affected by the geometry change rather than assuming a manufacturing improvement is mechanically neutral.
- 8. Close the loop with the intended manufacturer: Review stock form, cutting strategy, workholding, setups, tools, tolerance capability, deburring, finishing, inspection, and production quantity with the shop or supplier that will actually make the part.
The “after DFM” bracket is an instructional concept, not a released design. A real bracket still requires load, stiffness, fatigue, interface, tolerance, material, fastener, vibration, manufacturing, and inspection checks appropriate to its service.
DFM Is Not the Same as Cost Cutting
A DFM change is successful only when it reduces unnecessary manufacturing burden while preserving the requirements that make the product work.
Reducing machining time, tooling complexity, material usage, part count, or inspection effort can be valuable, but none of those goals automatically outranks function. A locating feature should not be removed if it controls repeatable assembly. A bearing seat should not receive a looser requirement if that permits unacceptable misalignment. A rib should not be deleted if stiffness or vibration performance depends on it.
Simplify geometry
Best fit: Features whose shape does not materially affect load path, interface, motion, sealing, clearance, appearance, or another requirement.
Tradeoff: Removing material or changing section geometry can alter stiffness, stress concentration, vibration, thermal behavior, and durability.
Do not use when: The geometry being removed performs a verified engineering function.
Relax tolerances
Best fit: Dimensions where additional variation does not threaten fit, alignment, motion, sealing, appearance, inspection, or reliability.
Tradeoff: More manufacturing freedom can reduce process burden, but excessive variation can consume assembly margin.
Do not use when: The tolerance is required by a verified functional stack, interface, or acceptance criterion.
Change manufacturing process
Best fit: When volume, geometry, material, tooling investment, lead time, or production rate makes another process more attractive.
Tradeoff: The process change may require different geometry, tolerances, material condition, surface treatment, tooling, validation, and supplier capability.
Do not use when: The proposed process cannot meet a mandatory material, performance, quality, regulatory, or production requirement.
Combine parts or features
Best fit: Where integration removes unnecessary handling, joining, alignment, inventory, or manufacturing steps.
Tradeoff: Integration can make replacement, inspection, tooling, material selection, service, or individual feature manufacture more difficult.
Do not use when: Separate parts are required for assembly, maintenance, material differences, adjustment, process access, or lifecycle replacement.
Production volume can change the correct answer
A process that is unattractive for one prototype may become economical for repeated production, while dedicated tooling that makes sense at high quantity may be difficult to justify for a handful of parts. Production rate, tooling life, setup time, material utilization, automation, quality requirements, supply-chain risk, and expected design changes all influence the decision. Use actual supplier and project data instead of assuming one manufacturing route is always cheaper.
Higher precision is not automatically higher quality
Quality means satisfying the product’s requirements consistently. Precision beyond the functional requirement can add manufacturing and inspection burden without creating additional product value. Conversely, loosening a requirement below what the assembly or function needs is not DFM—it is an undercontrolled design.
ASME’s DFM guidance frames the objective around manufacturing economically without sacrificing functionality and performance and highlights the interaction among materials, tooling, tolerances, manufacturing collaboration, and testing.
Final Design for Manufacturing Checklist Before Release
Use this final gate after the design has been reviewed for function and a realistic manufacturing route has been identified. A “no” answer should lead to a specific engineering or manufacturing action rather than an assumption that production will solve the problem.
- Functional requirements are protected: The team can identify the surfaces, features, tolerances, material properties, and interfaces that directly control performance.
- The manufacturing process is defined: The likely machining, molding, forming, casting, additive, fabrication, or other route is known well enough to assess the geometry.
- Production quantity is understood: Process and tooling choices reflect prototype, low-volume, or production needs rather than an undefined future quantity.
- Material and stock form are realistic: Material condition, availability, starting stock, treatments, finishing, joining, and supply constraints have been considered.
- Process-sensitive geometry has been reviewed: Tool access, draft/release, bends, cores, support removal, weld access, machining allowances, or other applicable process constraints are addressed.
- Workholding and fixture access are credible: The part can be located and restrained through the required operations without relying on inaccessible or unstable surfaces.
- Unnecessary setups have been challenged: Every additional orientation or secondary operation has a functional or manufacturing reason.
- Tolerances are function-driven: Critical requirements are controlled deliberately, while noncritical features are not burdened with unjustified precision.
- Datum strategy supports manufacturing and inspection: Critical geometric relationships can be established and verified consistently.
- Surface requirements are intentional: Finishes and cosmetic controls are applied where function or product requirements justify them.
- Inspection is feasible: Required features are measurable using an appropriate, repeatable production inspection method.
- Secondary operations are identified: Deburring, cleaning, finishing, coating, heat treatment, joining, post-processing, inspection, and marking are understood where applicable.
- Assembly implications have been checked: DFM changes have not created a handling, fastener, orientation, alignment, access, or service problem downstream.
- Engineering consequences of geometry changes were rechecked: Relevant stress, stiffness, fatigue, vibration, thermal, wear, sealing, or other analyses reflect the revised geometry.
- Actual manufacturer capability has been confirmed: Critical assumptions are supported by supplier, equipment, tooling, inspection, or process information rather than generic capability claims.
- Open manufacturing risks have owners: Unresolved process questions are documented with a planned prototype, trial, inspection, supplier review, or verification activity.
Do not release a design merely because the CAD model and drawing are complete. Hold release when a critical feature cannot be manufactured or inspected as defined, the manufacturing route is still incompatible with the geometry or material, supplier capability is unresolved for a critical requirement, or a DFM change has not been checked against the product’s actual engineering requirements.
DFM is one part of the larger mechanical engineering design process. Once individual parts are manufacturable, the logical next review is often Design for Assembly, followed by verification that the manufactured and assembled product meets its controlled requirements.
Design for Manufacturing Engineering References
These sources support the manufacturability-analysis, early manufacturing involvement, and practical DFM principles used on this page. Process-specific limits still depend on the selected material, manufacturing route, tooling, supplier capability, and applicable project requirements.
- National Institute of Standards and Technology — Automated Manufacturability Analysis: A Survey NISTIR 5713, published 1995 — supports identifying manufacturing problems during the design phase and providing manufacturability feedback before production.
- MIT OpenCourseWare — Lecture 12: Design for Manufacture Spring 2010 course material — provides educational context for incorporating manufacturing considerations during product design.
- ASME — How to Apply Design for Manufacturing Principles to Your Project Published March 31, 2023 — supports the interaction among function, manufacturing cost, materials, tooling, tolerances, production collaboration, compliance, and testing.
- ASME — Pulse of the Profession: Design for Manufacturing Published April 15, 2023 — supports integrating manufacturing engineering into the design process instead of treating production feedback as a late-stage handoff.
Frequently Asked Questions
What is the difference between design for manufacturing and manufacturability?
Design for Manufacturing, or DFM, is the design activity used to improve how a product will be produced. Manufacturability describes how feasible and practical the resulting design is to manufacture under a particular set of process, equipment, material, quality, volume, and supplier conditions. “Design for manufacturability” is also commonly used as an expanded form of DFM.
When should a DFM review be performed?
Manufacturing constraints should begin influencing the design while major process and geometry decisions are still changeable. A more detailed DFM review should occur before production drawings, tooling, supplier commitments, and release decisions make redesign expensive. Manufacturing feedback should continue as prototypes and production evidence reveal new information.
Does DFM mean using the loosest possible tolerances?
No. DFM means using tolerances that protect function while avoiding precision that does not create functional value. Critical fits, alignment, sealing, motion, geometric relationships, or assembly requirements may need tight control. The correct tolerance comes from the functional requirement, tolerance stack, process capability, and inspection method.
Is DFM only for high-volume products?
No. DFM matters for prototypes, one-off equipment, and low-volume components because difficult tooling, inaccessible features, excessive setups, special processes, or poor inspection access can still add cost and schedule. Production quantity changes which tradeoffs matter most; it does not eliminate the need to consider manufacturing.